Progressive Metal Stamping
Repeat parts made with progressive dies in Southington, Connecticut, from short runs to ongoing production programs.
12
Progressive Press Lines
45–150
Ton Progressive Press Range
.005″–.250″
Material Thickness
14″
Maximum Strip Width
Progressive Stamping, Short Run to High Volume
Companion Industries has run progressive stamping in Southington, Connecticut since 1972. Two production shifts produce more than 100 million parts a year, with toolmakers on hand for die adjustments and repairs.
Need to prove out a part before committing to a progressive die? With wire EDM, CNC machining, and commercial 3D printers in house, we make prototype parts and test the tooling approach first. We have done this for some of our largest customers.
Explore exotic metals, specialty alloys, and pre-finished coil stock
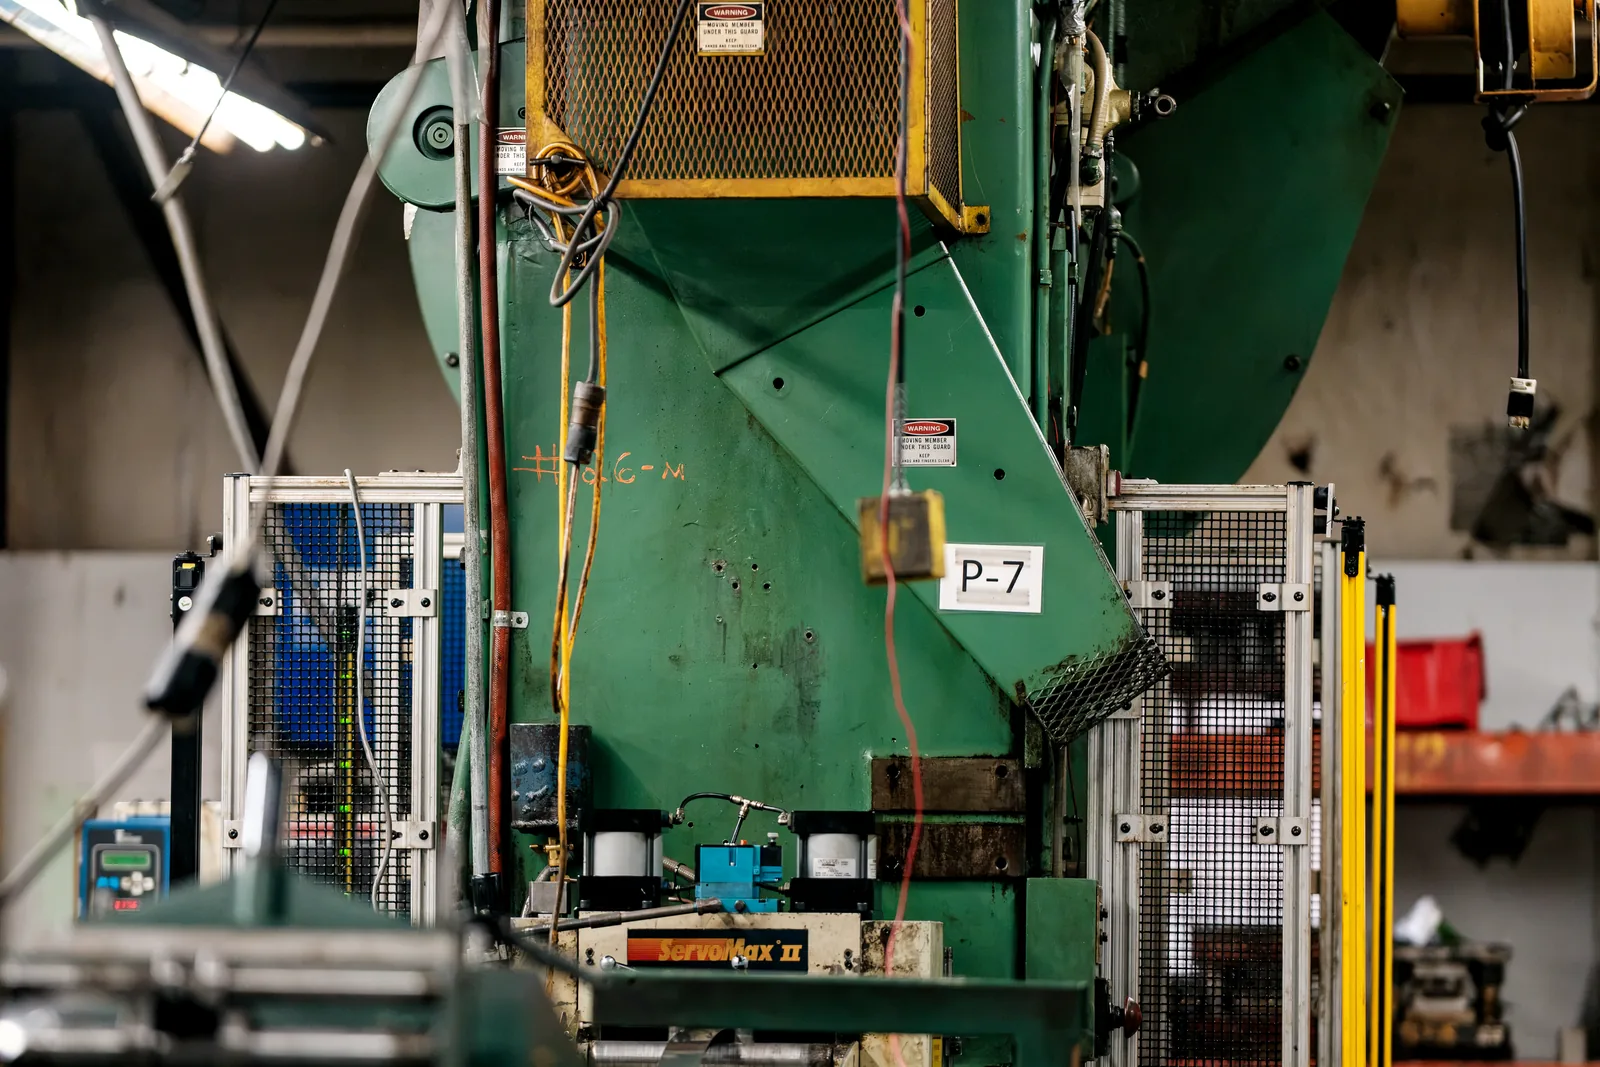
Metal Stamping in Motion
A closer look at the tooling and material feed equipment running in our press room.
Inside the Stamping Press
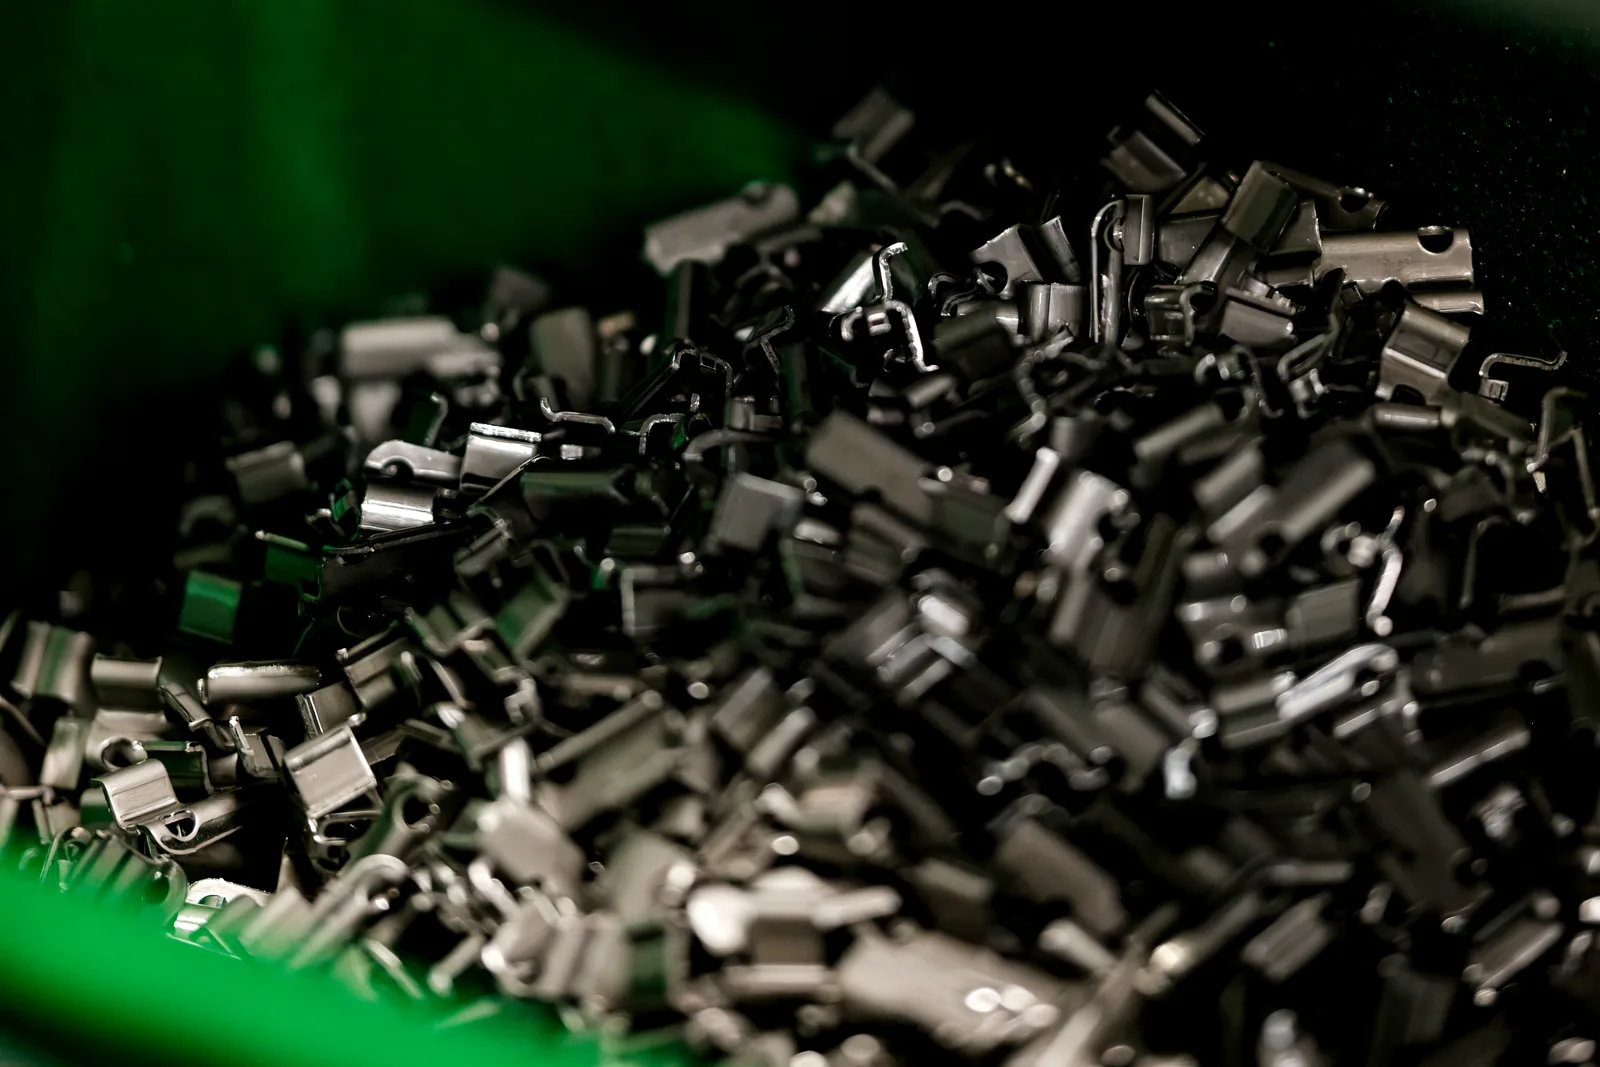
Close-up views of the dies cycling and stamped parts leaving the tooling.
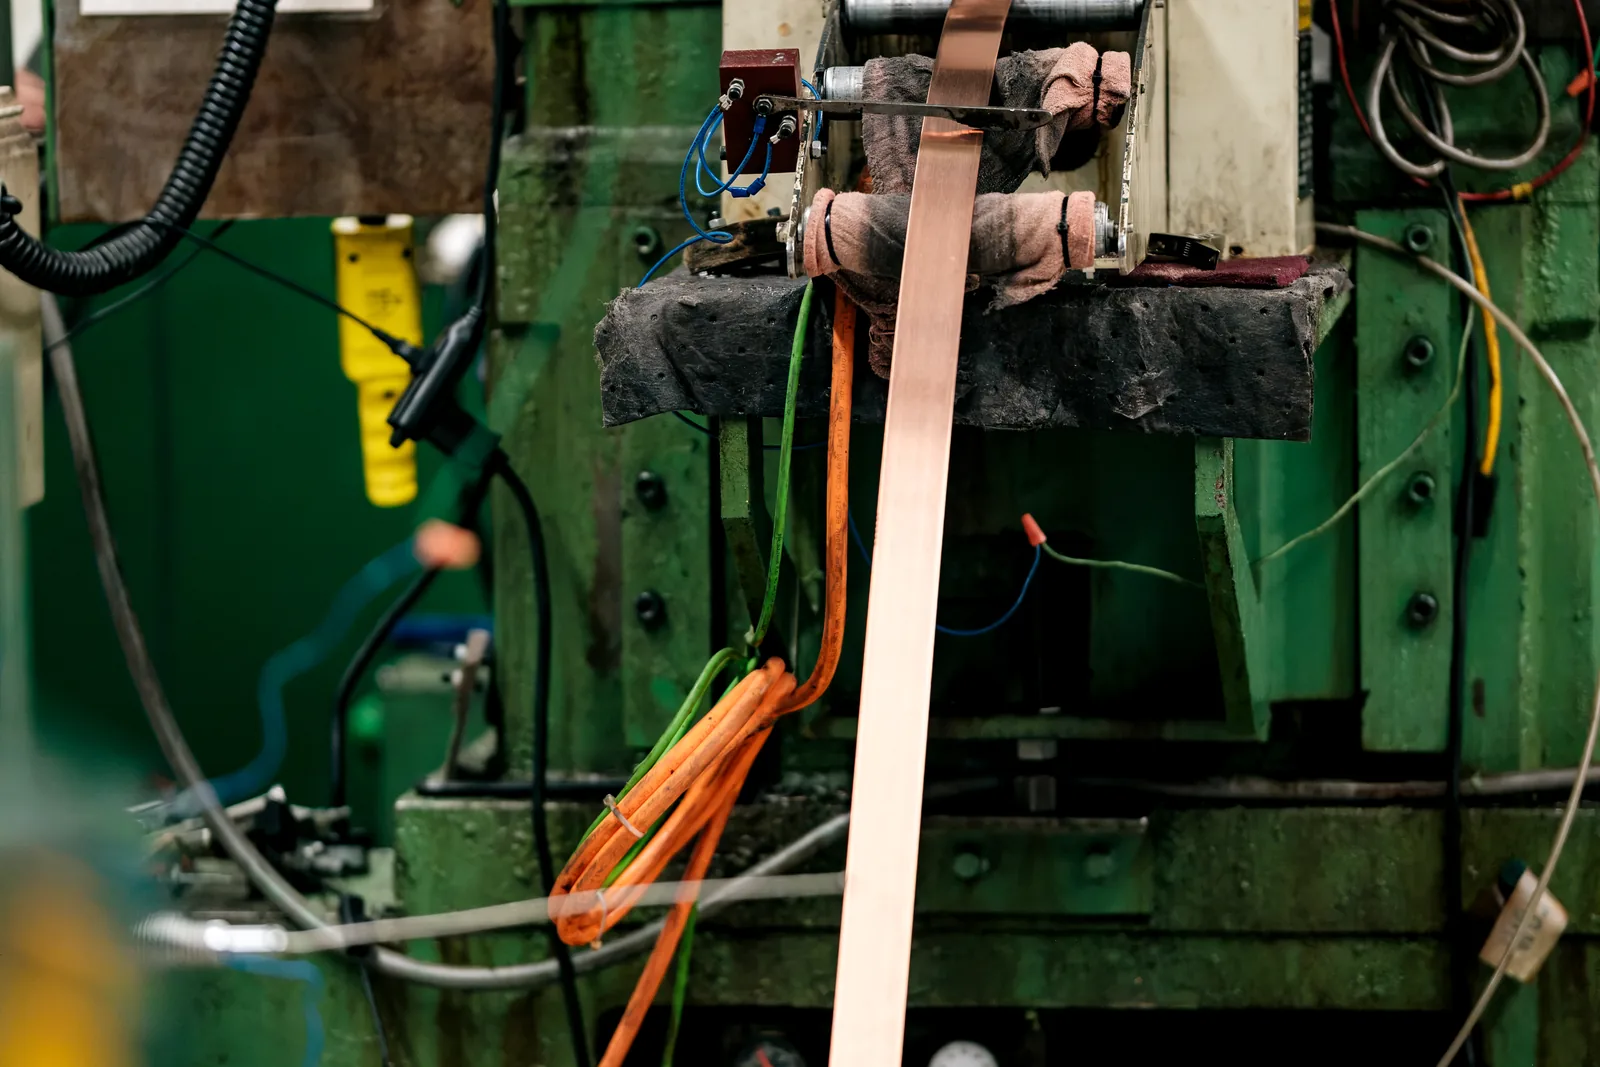
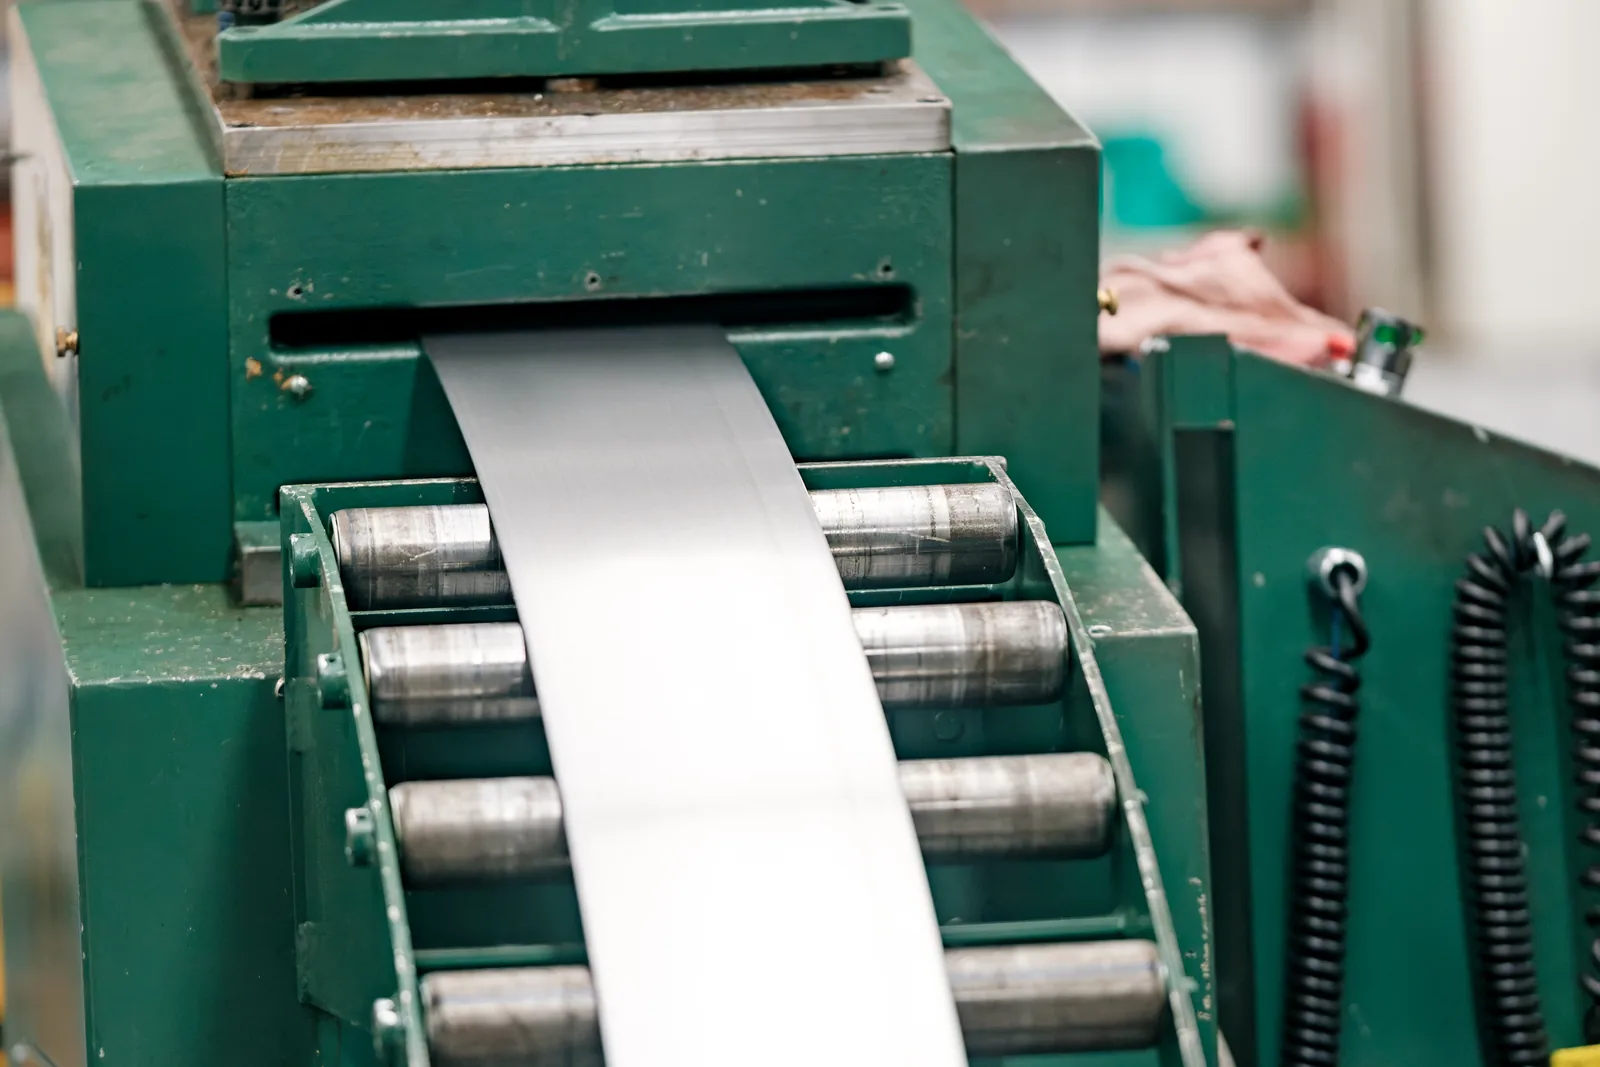
Coil & Strip Feeding
Coil unwinding and strip advancing through the feed equipment, shown from three angles.
Metal Stamping Capabilities
Progressive Die Stamping
Multi-station progressive dies for high-volume, complex geometries with tight tolerances and repeatable quality.
Short Runs & Repeat Orders
Small batches to check fit and function, followed by production releases planned around your quantities and timing.
Multi-Material Expertise
Experience across dozens of materials and grades, including steel, stainless steel, aluminum, copper, brass, and specialty alloys. We work to your application and material specifications.
In-House Tooling
Toolmakers work with stamping operators on die adjustments, maintenance, and repairs throughout a production program.
Secondary Operations
Fourteen secondary presses up to 75 tons, plus tapping, deburring, riveting, spot welding, and laser marking to deliver complete parts.
Quality Built Into Production
Operators check parts during the run against a documented inspection plan and record the results.
Stamping Equipment & Specifications
Progressive stamping presses
- Minster 150 ton press (1)
- Minster 100 ton presses (3)
- Minster 75 ton press (1)
- Minster 60 ton presses (4)
- Titan TNI-60 60 ton press (1)
- Minster 45 ton press (1)
- Minster No. 6 OBI press (1)
Coil handling
- Servo roll press feeds (14)
- Coil straighteners (12)
- Stock reels, power reels, and decoilers (12)
- Coils up to 5,000 lb
- Strip up to 14″ wide (150 ton press)
Materials
- Steel, stainless steel, aluminum, copper, brass, and specialty alloys
- Material thickness .005″ to .250″
Supply programs
- Blanket orders
- Safety stock
- Kanban & JIT releases
- Bar coding
Equipment list current as of October 2026. Download the full line card (PDF)
A vendor network built through experience
The outside services your part needs
A part may need several processes after stamping or machining. We coordinate those steps through a vendor network with experience across a wide range of cleaning, inspection, heat treating, plating, and coating requirements.
We plan outside services alongside tooling, production, and assembly, with your drawing and process specifications guiding the work.
Deburring & cleaning
- Deburring & tumbling
- High Energy Tumble
- Cleaning
- Ultrasonic cleaning
- Vacuum cleaning
Inspection & heat treatment
- Fluorescent penetrant inspection (FPI)
- Passivation
- Belt heat treating
- Vacuum heat treating
- Bright annealing
Plating
- Rack plating
- Nickel & electroless nickel
- Dull tin
- Silver & gold
- Brass
Coatings & surface finishes
- Bronze coating
- Dry film, Teflon & Slickshot
- Powder coating & painting
- Black oxide & manganese phosphate
- Alodine & anodizing
Need a process you don’t see here? There’s a good chance we’ve worked with it. Tell us what your part requires.
Progressive Metal Stamping FAQ
How do you confirm a part will fit your presses?
Send the part drawing and any existing tool dimensions. We review the geometry and tooling against the press requirements; press bed sizes are available on request.
What material details do you need to review a stamping?
Include the material specification, thickness, and temper on your drawing so we can review them against the part geometry.
Can you run stamping dies we already own?
Yes. Customer-supplied tooling is welcome. Our toolroom can review the condition of an existing die and handle maintenance, repair, or reverse engineering when it is needed.
Related Capabilities
Have a part to stamp?
Include material, stock thickness, annual volume, and target timing. We respond within 1 business day.